Choosing an acetone drum pump is not a minor purchasing detail. It affects transfer speed, operator handling, equipment life, and the chance of leaks around a busy work area. Acetone is a volatile solvent, so buyers should check that wetted materials suit the fluid and that the pump’s design matches the task. A drum’s size matters, too. A pump that works well with a small container may feel awkward beside a tall, frequently used drum. Small details count.
This guide compares seven options for industrial buyers, from manual pumps to powered models. It considers construction materials, flow control, power needs, hose arrangements, and routine cleaning. The best choice depends on the actual setup, not a headline flow rate. Review the product documentation, confirm compatibility with the manufacturer, and consider how the pump will be stored between transfers. A specification sheet cannot reveal every maintenance headache. A short trial may uncover one.
A named expert quotation cannot be responsibly included without a verifiable source; inventing one would weaken this guide’s reliability. The practical question remains: “Will this pump transfer acetone reliably in the conditions where it will actually be used?” The seven selections ahead help buyers assess that question with care.
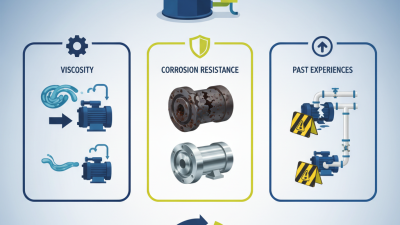
Acetone is a fast-evaporating, low-viscosity solvent. It can soften or damage plastics and seals that perform well with water. A drum pump must therefore be assessed by every wetted component, not just its outer housing. Stainless steel and PTFE are commonly considered for acetone service, but exact grades, seals, and operating conditions matter. Check the pump maker’s written compatibility data before purchase. A small compatibility chart is useful, but it is not a substitute for confirmation.
Pay close attention to the rotor, shaft, tube, gasket, and discharge hose. Some elastomers and plastics can swell, crack, or lose strength after prolonged contact. That failure may not be visible during a brief test. Acetone also produces flammable vapors, so buyers should select equipment rated for the application and follow site procedures for bonding, grounding, and ventilation. Keep the pump away from ignition sources. I would not assume a material is suitable based on one successful transfer; temperature, exposure time, and wear can change the result. Verify details with the supplier, then inspect seals regularly.
Selecting an industrial acetone drum pump starts with chemical compatibility. Check the pump tube, seals, hose, and fittings against the acetone supplier’s compatibility data. A mismatch can cause swelling, leaks, or premature wear. Small details matter. Do not assume that a metal tube makes every wetted component suitable. Seal materials can be the weak point. Confirm that the pump and motor are rated for the intended use around flammable vapors, and follow the equipment instructions for grounding and bonding. Keep transfer work in a well-ventilated area.
Match the pump to the drum opening, required lift, hose length, and expected transfer volume. A catalog flow rate is not a guarantee; restrictions and setup can reduce real-world performance. Fit matters. Consider how the pump will be operated, cleaned, and stored, especially if the same equipment handles different liquids. Review the full assembly, not just the pump tube. Before purchase, verify the materials, operating limits, and safety features with the manufacturer or a qualified safety professional. Even a careful shortlist may need revision after compatibility details are checked; that extra review is less frustrating than discovering a seal problem mid-transfer.
7 Best Acetone Drum Pumps for Industrial Buyers
Design matters when choosing among seven acetone drum pump types. A hand-operated rotary pump suits small, occasional transfers, while a lever pump offers simple control for measured dispensing. Both depend on operator effort. For frequent use, an air-operated diaphragm pump can move liquid without an electric motor at the drum. Its diaphragms and seals still need verified acetone compatibility.
Electric drum pumps can provide faster, steadier transfer, but the motor and installation must be suitable for the intended flammable-liquid service. A stainless-steel immersion pump may handle routine movement from drums into process vessels; check wetted parts and seals, not just the metal tube. Peristaltic pumps isolate liquid inside tubing, which can simplify cleaning, though tubing compatibility may rule them out. Small detail, big consequence.
A piston-style transfer pump offers controlled delivery for smaller batches, while diaphragm designs can better accommodate varied flow demands. Actual performance varies by model, viscosity, hose length, and lift height. Acetone also evaporates quickly, so closed connections, ventilation, and appropriate static-control measures matter during transfer. There is no tidy universal winner. Compare the pump’s documented material compatibility, duty cycle, and site requirements before selecting it; a familiar-looking seal is not proof.
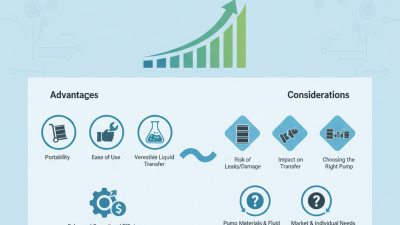
A qualitative guide to how common pump designs may fit typical acetone-transfer tasks.
How to read this chart: Application-fit scores are an editorial screening guide, not measured performance data or product ratings. Actual suitability depends on the pump’s wetted materials, seals, operating conditions, and relevant hazardous-area approvals.
Safety: Acetone is highly flammable. Confirm chemical compatibility and follow site requirements for grounding, bonding, ventilation, and ignition-source control.
Before installing an acetone drum pump, confirm that its wetted parts, seals, hose, and fittings are rated for acetone. A pump suitable for water may soften, swell, or leak when exposed to this solvent. Place the drum on a stable surface in a well-ventilated work area, away from heat, sparks, and open flames. Check the drum and pump for damage, then follow the equipment instructions for assembly and grounding or bonding. Small details matter.
Keep the pump outlet secured over the receiving vessel before starting transfer. Wear suitable eye and skin protection, and avoid breathing concentrated vapors. Operate the pump at a controlled rate; fast flow can cause splashing and static buildup. Never leave a transfer unattended. If a connection drips, stop the pump and address the leak using the site’s spill procedure. A tidy setup helps, but it is not a substitute for inspection.
After use, drain and handle the pump as its instructions specify, and close the drum promptly. Do not assume a pump is safe because it worked yesterday; seals and hoses can wear without obvious warning. Review the safety data sheet and workplace procedures before changing solvents or equipment. Even a careful checklist can miss a worn gasket, so inspect the parts that contact acetone before each shift.
An acetone drum pump is only as dependable as its wetted parts and daily checks. Confirm that the pump tube, seals, hose, and discharge fittings are rated for acetone; appearance alone proves little. Follow the pump instructions and the fluid’s safety data sheet when setting cleaning and handling steps. Acetone evaporates quickly. Residue can be difficult to spot. Keep the area ventilated, control ignition sources, and follow site procedures for bonding and grounding compatible equipment.
Before use, inspect the tube for cracks, the hose for soft spots, and connections for leaks. Check that the pump starts and stops correctly, with no unusual vibration or noise. After transfer, drain remaining liquid into a compatible, closed container. Clean the pump only as its manufacturer directs, and keep solvents away from electrical components. Replace damaged seals promptly. A rushed inspection can miss a small leak, so pause and check again if anything seems unusual.
Tips: Keep a dated inspection log. Note seal changes and cleaning dates. Store the pump dry, with its hose protected from kinks. Review your checklist periodically; a checklist can become stale when equipment or work practices change.
| Pump Option | Typical Wetted Materials | Best-Suited Use | Cleaning and Inspection | Maintenance Priorities | Acetone-Specific Selection Checks |
|---|---|---|---|---|---|
| 316 stainless steel electric vertical drum pump | 316 stainless steel tube; PTFE seals or gaskets where specified for the selected model. | Routine transfer from standard drums when an electric drive and a compatible pumping assembly are required. | Drain the tube after use. Flush only with a process-approved, compatible fluid; inspect the tube, outlet, and seal area for residue or leaks. | Check shaft condition, seals, couplings, and motor connections according to the pump manual. Replace worn seals with materials approved for acetone. | Confirm the complete wetted-material list and the motor’s suitability for the classified area. Bond and ground the drum, pump, and receiving container as required by site procedures. |
| 316 stainless steel air-driven drum pump | 316 stainless steel tube with acetone-compatible seals; air-motor materials are generally outside the wetted path. | Drum transfer where a pneumatic drive is preferred, such as locations where electric equipment requires additional area-classification review. | Depressurize and isolate the air supply before cleaning or inspection. Drain the liquid path and check the air connection for leaks or damage. | Inspect the air motor, regulator, hose, fittings, and muffler. Follow the maker’s instructions for lubrication and seal replacement. | A pneumatic drive does not eliminate static-ignition risk. Verify grounding, bonding, ventilation, and the pump’s pressure and flow limits. |
| 316 stainless steel air-operated double-diaphragm (AODD) drum pump | 316 stainless steel liquid-contact parts with PTFE diaphragms and compatible valve components, as specified by the pump supplier. | Transfer where self-priming capability, variable flow, or handling of occasional entrained air is useful. | Flush the liquid chambers using an approved procedure. Inspect diaphragms, ball valves, seats, and manifolds for swelling, cracking, or leakage. | Keep an inspection schedule for diaphragms and check air consumption, exhaust, and fasteners. Replace matched diaphragm sets when required. | Confirm diaphragm and valve compatibility, discharge pressure limits, and whether the pump can be drained fully. Control air pressure to the specified operating range. |
| Conductive PTFE-lined AODD drum-transfer setup | PTFE-lined liquid passages with conductive or grounded construction where available; elastomers and valve materials must be selected for acetone service. | Applications needing broad chemical resistance from the liquid-contact lining, subject to the pump’s full material and electrical specifications. | Use a compatible flushing procedure and inspect the lining, joints, and ports for damage, leakage, or signs of delamination. | Check diaphragms, valve components, fasteners, and the continuity of any conductive elements in line with the manufacturer’s instructions. | Do not assume a PTFE lining makes the entire assembly electrically conductive or suitable for a hazardous location. Verify grounding and area suitability. |
| 316 stainless steel positive-displacement gear pump | 316 stainless steel or other explicitly approved metal parts; PTFE-compatible sealing components as specified. | Controlled, steady transfer in a fixed installation when the pump is designed for low-viscosity liquid service. | Drain and flush the pump and connected piping using an approved method. Inspect the shaft seal, inlet, and discharge for leakage or blockage. | Monitor seal condition, gear wear, and operating noise. Use a correctly set pressure-relief arrangement where required for a positive-displacement pump. | Check the manufacturer’s minimum inlet pressure, speed, seal compatibility, and dry-running limits. Acetone’s low viscosity can affect leakage and lubrication assumptions. |
| 316 stainless steel hand-operated rotary drum pump | Metal liquid-contact components with seals specifically confirmed as suitable for acetone. | Small-volume or intermittent transfer where manual operation is acceptable and the pump is expressly approved for the liquid. | Drain the pump after use and clean it using a compatible procedure. Inspect the barrel connection, handle, shaft, and seals before each use. | Check for binding, corrosion, loose fittings, and worn seals. Store clean and dry in accordance with the site’s chemical-handling procedure. | Manual operation is not automatically ignition-safe. Bond and ground conductive equipment as required, and use only in an appropriately assessed area. |
| 316 stainless steel high-flow centrifugal drum pump | 316 stainless steel wetted parts with seals and impeller materials verified for the selected model and acetone service. | Higher-throughput transfer where the liquid is clean and the installation can maintain the pump’s required operating conditions. | Flush and drain the liquid path after transfer. Inspect the impeller, tube, outlet, and seal area for deposits, damage, or leakage. | Check impeller wear, shaft alignment, bearings, and seals. Avoid running the pump dry or outside its specified operating range. | Verify the pump curve against the actual lift, hose length, and flow requirement. Confirm motor area suitability and static-control measures before use. |
Selection note: These are generic pump configurations, not specific product endorsements. Acetone is a highly flammable solvent. Before purchase or operation, verify every wetted material against the pump manufacturer’s acetone compatibility data, review the site’s hazardous-area requirements, and follow applicable grounding, bonding, ventilation, and handling procedures.
![]() |
Need Help? Call Us 203-740-1877
|
We're ready to help identify, size and spec your pumps, filters |
Pumps, Parts, and Equipment – Guidance Included
103 Hempel Drive
Wolcott, CT 06716
Telephone: 203-740-1877
Toll Free Fax: 866-523-1693
Email: sale@rewritertool.com